جدول المحتويات
Water Tank Weld Inspection should be treated as a system decision. Its purpose is to match inspection methods and acceptance criteria to the welded tank material, joint function, and project specification. Across engineering, procurement, construction, and operations, approval requires more than finding the right label; the complete arrangement must work across the expected operating range.
Poor water tank weld inspection creates a predictable risk: A visual check performed without defined criteria cannot confirm every weld characteristic required by the design. A structured review makes the risk easier to find and manage. The responsible engineer and the applicable project rules remain the final authority. It organizes the questions that require documented answers, which interfaces require coordination, and what evidence should remain at handover.
Why Water Tank Weld Inspection Deserves an Early Review
The right stage to settle water tank weld inspection is early enough to avoid field rework. During that review, visual inspection scope, surface or volumetric examination, and inspection timing can still be resolved before procurement, fabrication, or site execution. Deferring the decision can turn a design issue into field improvisation. The installer may not own the process or structural design basis.
Treat water tank weld inspection as a controlled item in the project interface register. All parties responsible for tank supply, connected systems, and operation must contribute information before the detail is complete. The industrial water tank buying checklist provides a useful companion review for commercial and technical scope boundaries.
Define the Operating and Design Basis
A credible water tank weld inspection decision requires agreed assumptions before hardware is selected. Define routine service before considering exceptions, the credible abnormal cases, environmental conditions, maintenance expectations, and the authority responsible for acceptance. When the data is provisional, record the assumption and the person who must close it.
- Welding code and project specification
- Base and filler materials
- Joint category
- Welder qualifications
- Inspection hold points
- Required nondestructive examination
A guessed allowance cannot repair a weak design basis. For water tank weld inspection, an incorrect flow, level, load, material, or service assumption can change the preferred arrangement. The revision trail deserves attention because a drawing based on an earlier data sheet can look complete while answering the wrong operating case.
Map Every System Interface
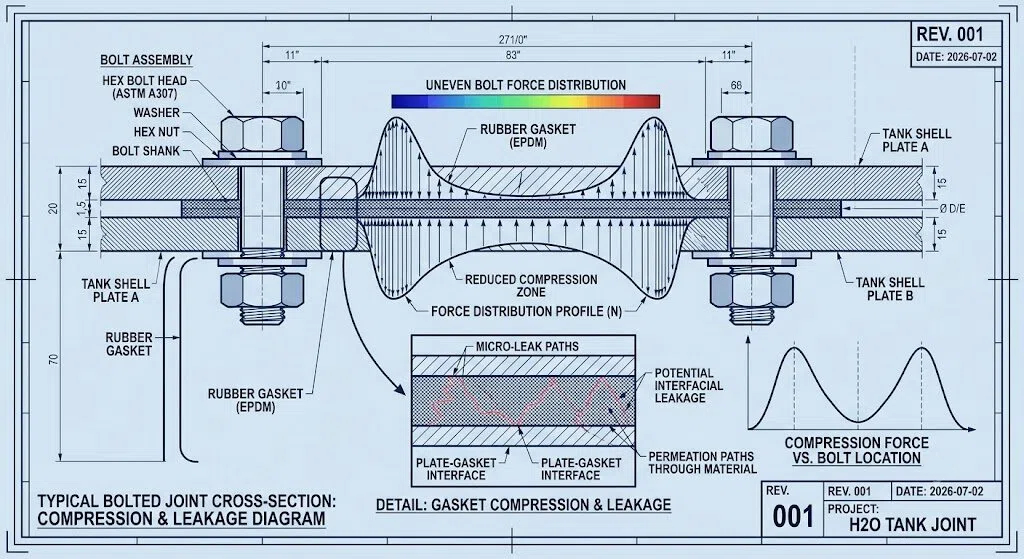
Several engineering scopes converge at the tank connection. Review water tank weld inspection against the inlet, outlet, overflow, drain, vent, level instruments, foundation, access system, and external piping as applicable. A change in one item may affect usable capacity, cleaning access, pipe loads, sanitary protection, or the sequence used to isolate the tank.
Keep elevations on one agreed datum and manage the nozzle schedule as a controlled record. P&IDs describe function; general arrangements describe location; structural drawings describe support; electrical documents describe control; and operating procedures describe use. The industrial water tank installation guide helps teams connect those documents to site and erection checks.
Key Water Tank Weld Inspection Decisions
The technical package should close each of these points for water tank weld inspection. Capture each decision in a controlled project document. An answer such as “by others” is only useful when the boundary and required input are also stated.
- Visual inspection scope
- Surface or volumetric examination
- Inspection timing
- Repair procedure
- Weld mapping
- Final documentation
When the shortlist contains two credible approaches, compare them against operation and maintenance rather than initial convenience alone. Good water tank weld inspection makes isolation, observation, cleaning, replacement, and inspection possible without transferring avoidable risk to the operator.
Materials and Service Compatibility
Material selection must reflect the stored water, temperature, cleaning method, exposure, and service conditions. In potable-water work, certification scope needs to be checked for the actual wetted coating, gasket, sealant, fitting, and component; one compliant part does not automatically establish compliance for the assembled system.
Coordinate water tank weld inspection with the selected tank construction. Details that work on a welded shell may not transfer directly to sectional or bolted panels. Review product-specific interfaces on the enamel water tank page, then confirm the project specification, approved material schedule, and supplier drawings.
Installation, Access, and Maintainability
A properly sized water tank weld inspection detail is incomplete without a workable installation and maintenance path. Reserve tool clearance, lifting space, valve reach, safe access, and room to remove screens, sensors, gaskets, or internal parts. Keep external pipe loads off tank connections unless the tank designer has explicitly accepted them.
Access planning must also respect the site’s safety program. Internal entry may be regulated as confined-space work, and roof or platform tasks may require specific fall-protection measures. Design the routine inspection from outside the tank wherever practical, then document any entry-dependent task and its isolation needs.
Common Failure Modes to Prevent
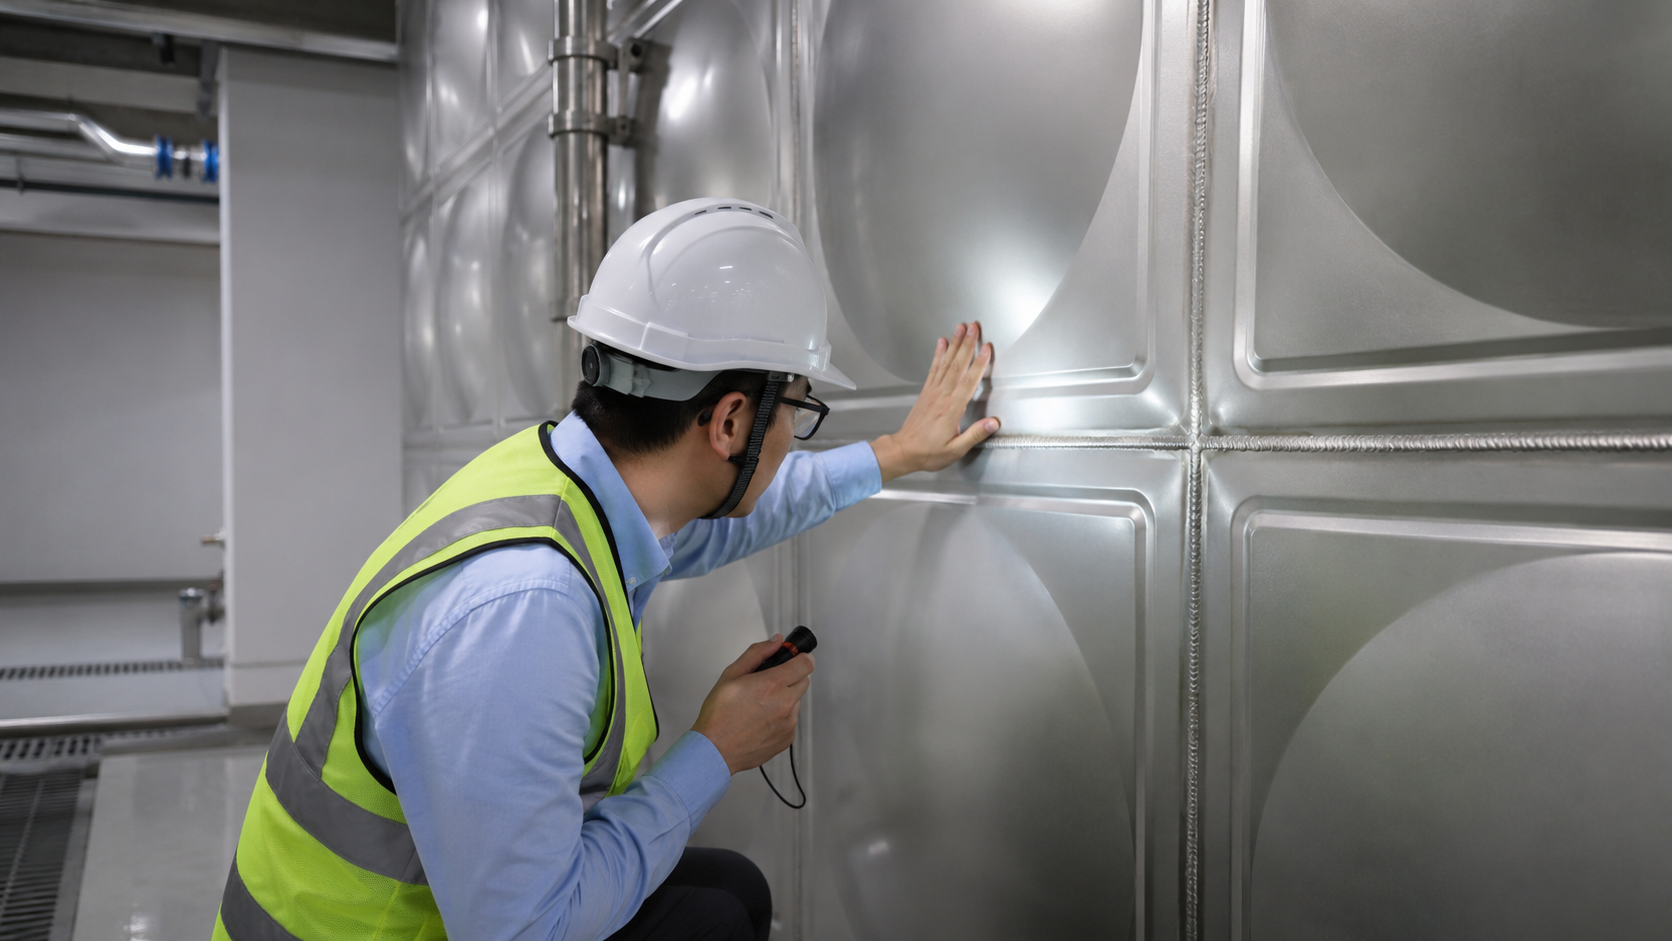
Testing the design against failure modes makes water tank weld inspection tied to observable project risks. Review the most likely causes, how they would be detected, and whether the system can be isolated without losing essential storage. The following issues deserve explicit discussion during drawing review:
- Inspection criteria chosen after welding
- Uncontrolled field repair
- Welds hidden before acceptance
- Passivation or coating applied over unresolved defects
None of these outcomes is prevented by a label alone. A sound water tank weld inspection package links the drawing to calculations, material data, installation instructions, inspection points, and an owner who will act on any nonconformance.
Water Tank Weld Inspection Review Table
| Review item | Question to close | Evidence to retain |
|---|---|---|
| Welding code and project specification | Confirm the project-specific value or arrangement for welding code and project specification. | Approved drawing, calculation, data sheet, or signed review record |
| Base and filler materials | Confirm the project-specific value or arrangement for base and filler materials. | Approved drawing, calculation, data sheet, or signed review record |
| Joint category | Confirm the project-specific value or arrangement for joint category. | Approved drawing, calculation, data sheet, or signed review record |
| Visual inspection scope | Confirm the project-specific value or arrangement for visual inspection scope. | Approved drawing, calculation, data sheet, or signed review record |
| Surface or volumetric examination | Confirm the project-specific value or arrangement for surface or volumetric examination. | Approved drawing, calculation, data sheet, or signed review record |
| Inspection timing | Confirm the project-specific value or arrangement for inspection timing. | Approved drawing, calculation, data sheet, or signed review record |
A completed table still needs calculations, drawings, and responsible approval. The value of a water tank weld inspection review is the traceable answer behind each row, including the responsible party and the revision where the answer was approved.
What to Put in the RFQ and Drawings
Bidders need a clear duty and an equally clear responsibility split. For water tank weld inspection, request enough information to compare bids on the same basis and to prevent a supplier assumption from becoming an installer problem.
- Design basis and applicable project requirements
- Tagged drawings with dimensions, elevations, and interfaces
- Material and component data
- Calculations or selection records required by the specification
- Installation, inspection, and testing instructions
- Deviation list and final handover documents
Do not allow exceptions to remain implicit. Silence should not be treated as proof that every requirement has been included. A complete water tank weld inspection submittal lets reviewers see what was selected, why it fits the duty, and what the site team must provide.
Verification Before Handover
Inspect the installed work against the accepted water tank weld inspection basis. Check identity, location, orientation, supports, materials, access, and associated controls before the tank is filled or returned to service. Where a functional test is safe and permitted, observe the result across the relevant operating range rather than only at one convenient point.
- Check qualifications and procedures
- Inspect fit-up and completed welds
- Review examination reports
- Trace repaired areas through final acceptance
Document what was measured, how it was observed, and what remains open. The finished water storage tank inspection guide و tank hydrostatic test roadmap can help place water tank weld inspection within the broader inspection and commissioning sequence.
Authoritative References
The final requirement comes from the project documents and applicable authority. The following public references are useful starting points for a water tank weld inspection review because they address tank operation, water quality, structural loads, fabrication safety, or inspection from recognized organizations:
- AMPP overview of coating holiday testing
- OSHA 29 CFR 1910.252 welding, cutting, and brazing
- OSHA 29 CFR 1910.146 permit-required confined spaces
- NSF/ANSI/CAN 61 testing and certification overview
- EPA finished-water storage inspection checklist
Every reference has limits that must be respected. A guidance document for public drinking-water storage may offer a helpful principle, but it does not automatically govern every industrial process-water tank. The responsible professional should reconcile water tank weld inspection with the project jurisdiction and contract documents.
الأسئلة الشائعة
When should water tank weld inspection be finalized?
Finalize water tank weld inspection before fabrication approval, after the process duty and site interfaces are stable enough for coordinated review. Later changes should follow formal change control.
Who is responsible for water tank weld inspection?
Responsibility is normally shared across the tank supplier and the process, piping, structural, controls, installation, and owner teams. The purchase specification should define each boundary.
Can a standard detail be used for water tank weld inspection?
A standard detail can be a starting point, but its flows, loads, materials, elevations, environment, and maintenance assumptions must be checked against the actual project.
What should be checked during commissioning?
Check the installed arrangement against the approved water tank weld inspection drawing, then verify supports, access, materials, controls, and any safe functional test required by the commissioning plan.
What records should be kept after handover?
Retain approved drawings, calculations or selection records, material data, inspection and test reports, setpoints, photographs, nonconformance closeout, and maintenance instructions.
Final Project Takeaway
Effective water tank weld inspection links process need, interface control, material selection, and field acceptance. That chain is more valuable than a generic detail because it remains understandable to the people who will operate and maintain the tank.
For a project-specific tank interface review, prepare the stored liquid, capacity, operating levels, site conditions, flow or load data, required standards, and preferred connection details. Then contact Zhengling so the technical discussion can begin with a defined water tank weld inspection basis rather than an incomplete equipment list.